

 Crown Win
Many brands focus solely on the end consumer when designing packaging, often overlooking the core needs of wholesale buyers.
This common oversight can lead to various pain points in the procurement process: packaging structures that are inconvenient for bulk storage, inconsistent quality across large batches, labeling that fails to meet regulations for cross-border distribution, and unit costs that are too high, squeezing wholesalers' profit margins.
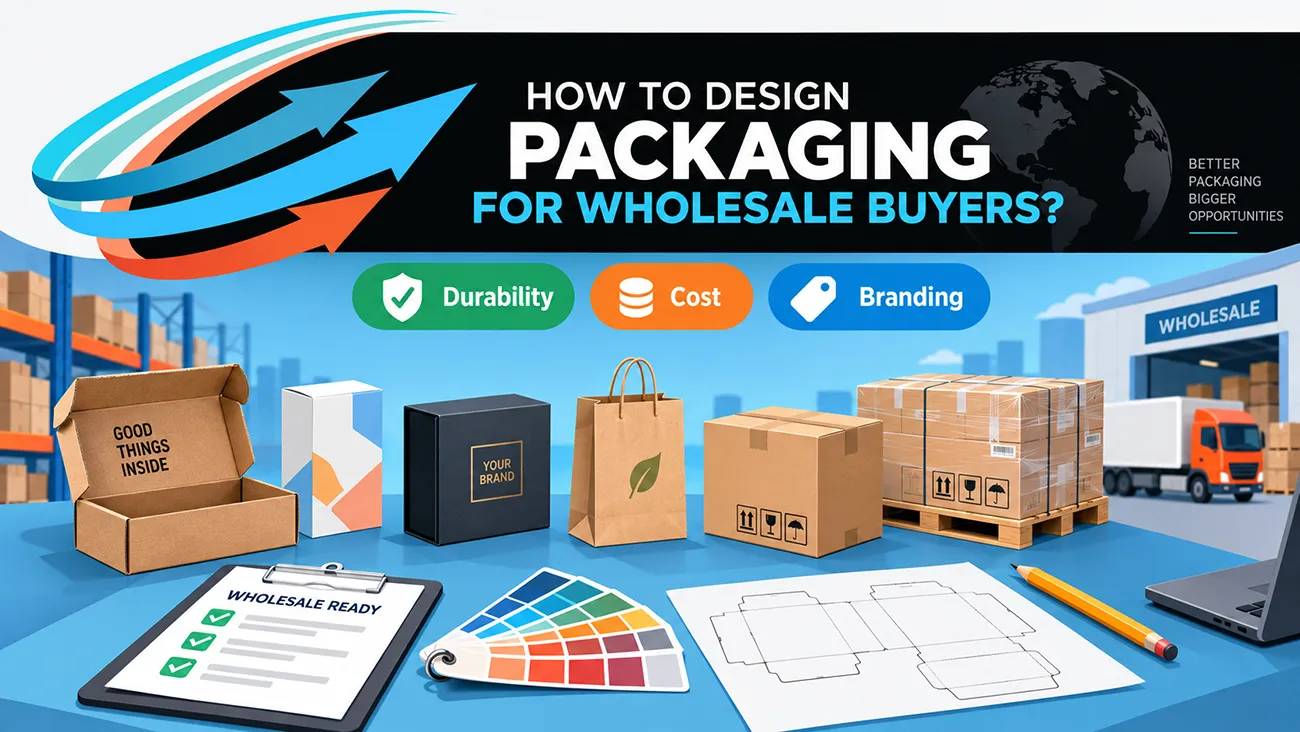
Unlike retail-oriented packaging, wholesale packaging requires a balance between aesthetics, cost control, stackability, export compliance, and production consistency. Well-designed, custom paper packaging for wholesale helps brands secure long-term partnerships, mitigate risks associated with large orders, and expand global distribution channels.
1. Prioritize Stackability and Storage Efficiency
Wholesale buyers typically purchase in large volumes for warehousing and secondary distribution, making structural practicality a top priority. Overly complex shapes, irregular dimensions, and bulky, rigid structures waste warehouse space and drive up shipping costs. Professional wholesale packaging utilizes standardized folding designs, uniform external dimensions, and compression-resistant paperboard materials.
This optimized structure allows for high stacking, reduces breakage rates in warehouses, and minimizes cargo volume for air and sea freight in cross-border shipping. Avoid over-engineered decorative structures; these add no value but increase logistics costs—a critical factor influencing a wholesale buyer's willingness to place repeat orders.
2. Balance Premium Aesthetics with Wholesale Cost Control
Wholesale buyers require packaging that maintains a premium brand image for resale while keeping the unit price competitive. Many brands either use cheap packaging that diminishes the product's perceived value or over-utilize complex finishing techniques, resulting in excessive wholesale costs.
The ideal solution for custom wholesale paper packaging is a streamlined premium design: retain core brand elements—such as precise logo printing and refined embossing—while eliminating redundant multi-layer finishes and utilizing standardized paper materials. This ensures a consistent brand image across retail channels and stabilizes unit prices, thereby maximizing profit margins for distributors.
3. Integrate Global Export Compliance to Facilitate Cross-Border Wholesale
Most overseas wholesale buyers distribute products across multiple regional markets, imposing strict requirements regarding packaging compliance. Non-compliant recycling symbols, uncertified paper materials, and incorrect regulatory information can lead to wholesale shipments being detained by customs, resulting in significant losses for distributors and brands.
Compliant wholesale packaging must meet EU PPWR, EPR, and FSC certification standards from the outset and feature standardized, compliant printed labels. Such packaging design enables the free circulation of wholesale products across European and North American markets, eliminating regional distribution barriers for buyers.
4. Ensuring Batch Consistency and Flexible Order Adaptability
Major pain points in wholesale packaging procurement include batch-to-batch color variations, inconsistent print quality, and long production lead times. Wholesale buyers require consistent packaging for long-term distribution while also needing the flexibility to place small-batch trial orders to test new markets.
Packaging designs must align with established mass-production processes—avoiding overly intricate techniques that are difficult to replicate at scale—and allow for parameter adjustments to accommodate fluctuations in order volume.
The Advantages of Crown Win Packaging’s Custom Solutions
As an export-oriented Chinese paper packaging manufacturer, Crown Win Packaging specializes in tailoring wholesale paper packaging for global brands and distributors. Our wholesale packaging solutions are designed with bulk logistics, cost control, and regulatory compliance in mind—prioritizing these factors alongside consumer aesthetics.
Our in-house quality control system ensures zero color variation and consistent quality across large wholesale orders. We support new brands with flexible, low-MOQ trial orders while providing fixed-batch production for long-term distributors. Leveraging our extensive export experience, we vet EU and international compliance standards during the design phase to mitigate customs risks. Furthermore, our standardized production scheduling guarantees stable lead times, helping wholesale buyers efficiently manage inventory and distribution plans.
Conclusion
Packaging design for wholesale buyers must prioritize practical logistics, cost control, cross-border compliance, and batch consistency—factors that distinguish it sharply from retail-focused packaging design. Effective wholesale packaging design enhances a brand's competitiveness within distribution channels and strengthens long-term B2B partnerships.
You can read our previous blog post, "Retail, E-commerce, and Gift Packaging: What’s the Difference?", to further optimize your multi-channel packaging strategy. If you require custom paper wholesale packaging solutions suitable for bulk export and distribution, please contact the expert team at Crown Win Packaging for free design guidance and project assessment.
 Inside the Custom Packaging Factory: From Paper to Finished Box